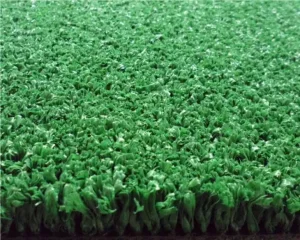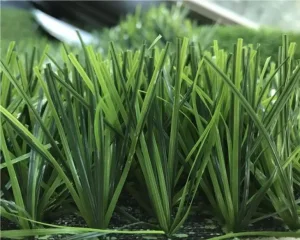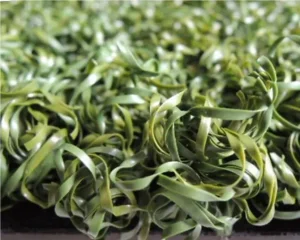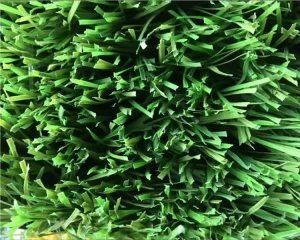
Featured Synthetic Turf & Coloured Fiber Systems
Engineered from raw polymer compound masterbatches to calibrated tuft matrices, our manufacturing floor delivers international tournament and high-durability architectural installations.
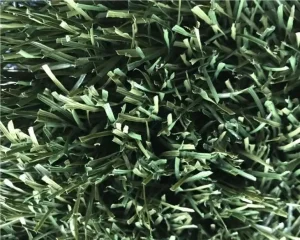
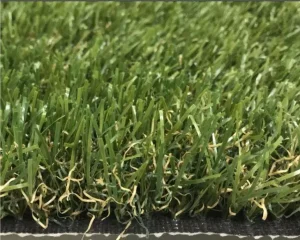
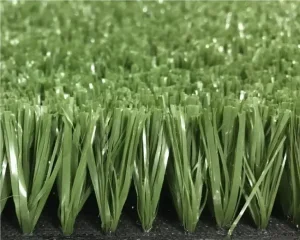
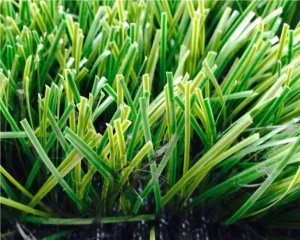
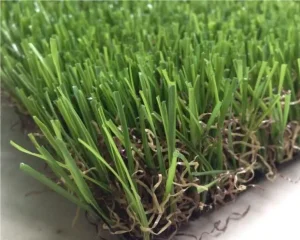
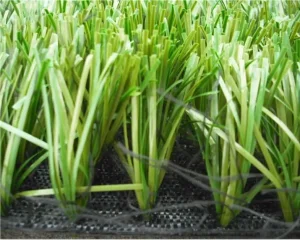
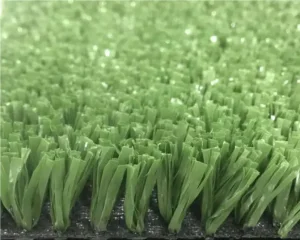
Technical Roadmap & Chromatic Polymer Evolution
Transforming coloured synthetic grass from aesthetic novelty to heavy-duty architectural and athletic grade requires breakthrough molecular stabilization, polymer blending, and automated tufting precision.
In-Dope Masterbatch Encapsulation
Traditional top-coating or dip-dyeing degrades under foot shear and UV radiation. Our state-of-the-art extrusion integrates virgin high-density polyethylene (HDPE) with non-heavy-metal inorganic pigments directly at melt-blown phase. This achieves molecular-level lock-in, guaranteeing ΔE < 1.5 color fastness through 5,000 hours of accelerated QUV weathering tests.
HALS Tri-Phase UV Thermal Shield
Coloured polymers—especially vibrant hues like signal red, royal blue, and optic yellow—absorb heat differently than standard chlorophyll greens. We implement a proprietary Hindered Amine Light Stabilizer (HALS) tri-phase additive package, dampening photo-oxidation, preserving tensile elongation, and mitigating thermodynamic surface degradation up to 70°C.
Multi-Axis Geometric Cross-Sections
Eliminating synthetic shine and directional matting through custom extruded blade cross-sections: C-Shape, W-Shape, and Diamond profiles. These geometric structures provide rapid elastic recovery under static compression, uniform omnidirectional ball roll, and anti-glare chromatic diffusion across varied sun angles.
Macro-Industry Solutions: Multi-Sector Applications
Coloured synthetic surfaces serve beyond decorative accents. They provide functional zoning, pedagogical stimulation, sensory safety, and multi-sport court boundaries.
K-12 & Early Childhood Education
Chromatically partitioned play zones incorporating integrated hopscotch, running tracks, and thematic learning hubs. Paired with non-toxic, lead-free, and shock-pad sub-bases ensuring critical fall height (CFH) compliance up to 3.0 meters under EN1177 safety criteria.
Multi-Sport Field Demarcation
High-density tufted colored lines (white, yellow, blue, red) permanently integrated during manufacturing. Eliminates painted lines that peel and requires minimal maintenance across hybrid tennis, paddle, hockey, and collegiate track setups.
Commercial Brand Identity & Retail
Bespoke tufted brand patterns, corporate emblems, and high-traffic wayfinding tracks for tech campuses, hospitality pool surrounds, experiential rooftop lounges, and flagship commercial retail environments.
Civic Infrastructure & Urban Greenery
Engineered medians, transit hubs, roundabouts, and drainage swales demanding zerowater maintenance, fire-retardancy (Class Bfl-s1), and rapid water evacuation (permeability > 60L/min/m²).
China Factory 4.0: Supply Chain Resilience & Scalability
Rooted in Taiwanese engineering management since 2002 and backed by RiThai's polymer heritage since 1977, our smart manufacturing clusters offer uncompromising quality control and unmatched scale.
Closed-Loop Vertical Synthesis
From masterbatch pigment formulation and monofilament yarn extrusion to high-precision tufting and secondary PU/Latex backing application, our fully integrated manufacturing loop removes third-party margin creep and guarantees roll-to-roll chromatic consistency.
AI-Powered Machine Vision QC
Industry 4.0 optical inspection scanners continuously monitor the tufting bed, identifying micro-shifts in stitch count, yarn tension imbalances, or chromatic deviations at full production speeds. This ensures ISO 9001, 14001, and 45001 compliance with zero defect escapes.
Buffer Storage & Logistics Network
Located adjacent to deep-water shipping lanes in Shanghai and Ningbo, our facility maintains raw polymer buffer inventories mitigating global supply chain turbulence. Direct intermodal links secure competitive sea freight quotes and expedited FOB/CIF handling for international contracts.
B2B Specification Guide for Coloured Synthetic Turf
Engineered to exceed municipal benchmarks, our fiber matrices are customized across pile configurations, polymer densities, and backing architectures.
| Target Segment | Fiber Polymer | Pile Height | Dtex & Gauge | Tuft Bind Force | Primary Backing & Secondary Coating |
|---|---|---|---|---|---|
| Pre-School Playgrounds | Soft PE Monofilament + PP Curled Thatch | 20 – 35 mm | 8,500 – 11,000 Dtex (3/8") | ≥ 40 N (High Tear Pull) | Dual Polypropylene Cloth + Polyurethane (Eco-PU) |
| Athletic Running Tracks | Texturized High-Density PP / PA | 13 – 18 mm | 9,000 – 14,000 Dtex (3/16" or 5/32") | ≥ 45 N (Stud Resilient) | Reinforced Anti-UV Fleece + SBR Latex |
| Multi-Sport Demarcation | UV-Resistant PE Diamond Monofilament | 40 – 60 mm | 12,000 – 16,000 Dtex (5/8" or 3/4") | ≥ 50 N (Heavy Impact) | Triple Multi-Layer Matrix + PU Compound |
| Commercial & Retail Zones | Matte Finish C-Shape Low-Glare PE | 25 – 40 mm | 7,500 – 9,500 Dtex (3/8") | ≥ 35 N (Foot Traffic) | UV Woven Scrim + Fire-Retardant Latex |
| Golf Fringe & Putting Target | Fibrillated / Curly Pure Polyamide (Nylon) | 10 – 15 mm | 6,600 – 8,800 Dtex (1/8" or 5/32") | ≥ 40 N (Precision Roll) | Dual Dimensionally Stable PET Weft + PU |
Global Compliance & Regional Import Support
Navigating regional testing standards and toxicological barriers is crucial for seamless institutional delivery. Our products come fully documented for immediate site clearance.
REACH & Non-PFAS Certification
Strict non-detection of per- and polyfluoroalkyl substances (PFAS) under EPA Method 537 / DIN EN 17681. Fully audited under EU REACH regulations, with testing covering over 230 Substances of Very High Concern (SVHC), RoHS non-heavy-metal compliance, and DIN 18035-7 environmental eco-toxicity requirements.
Fire Safety (EN 13501-1 Class Bfl-s1)
For high-density indoor public venues, commercial shopping atriums, and multi-story rooftop gardens, our coloured grasses can be produced with halogen-free flame retardants, passing EN ISO 9239-1 radiant panel combustion testing and generating minimal smoke emission.
End-to-End Import Assurance
We assist contractors, municipal tenderers, and commercial wholesalers with full documentation suites: Country of Origin (Form E, CO), custom tariff code harmonization (HS 5703.30), mill test reports, container load optimization plans, and specialized installation schematics.
Frequently Asked Technical & Sourcing Questions
Direct answers addressing technical parameters, minimum orders, customized pantone matching, and lifecycle performance.
Unlike cheaper alternatives that coat yarn surfaces, our factory blends automotive-grade pigments and multi-stage Hindered Amine Light Stabilizers (HALS) into virgin polymer chips before extrusion. This produces true in-fiber molecular color saturation, passing 5,000+ hours of ISO 4892-3 UV testing with negligible chroma loss.
For standard production shades (Signal Red, Navy Blue, Optic Yellow, Snow White, Jet Black, Purple), we support small project runs starting at 500 square meters. For custom Pantone matching requiring bespoke polymer extrusion batches, our baseline MOQ is typically 1,500 – 2,000 square meters.
Yes. We specialize in precision factory-level inlaying and CNC computerized tufting. This allows intricate play patterns, school mascots, agility fitness lines, and agility ladders to be embedded into rolls, drastically slashing on-site cutting, seam-taping labor, and joint failure risks.
In regions experiencing extreme temperature swings (such as the Middle East or southern US), standard SBR latex can contract or wrinkle. We recommend our high-grade dual-layer woven polypropylene backing backed by Polyurethane (PU) coating, which remains dimensionally stable up to 80°C and eliminates thermal seam stress.
Institutional & Multi-Purpose Systems Collection
Engineered systems engineered to balance abrasion dynamics, resilient pile memory, and strict municipal non-toxicity benchmarks.